How Wire-Laser Directed Energy Deposition works, how blue and infrared lasers compare, how it measures up against WAAM, electron beam and powder processes, which metals it prints and how to tell if it suits your parts.
Wire and lasers
Wire-Laser DED melts metal wire with lasers and deposits it layer by layer to build or repair parts.
A DED process
It belongs to Directed Energy Deposition in ISO/ASTM 52900, also written as DED-LB/w or W-LMD.
Control over speed
More control and resolution than wire arc (WAAM) and no powder handling, but slower deposition than WAAM.
Medium to large parts
Best for parts from about 50 mm to over 1 m, repairs and hybrid printing and machining.
What is Wire-Laser DED?
Wire-Laser DED is a metal additive manufacturing process that melts metal wire with lasers and deposits it layer by layer to build or repair a part. It belongs to Directed Energy Deposition (DED), one of the seven process families defined in the ISO/ASTM 52900 standard, where a focused energy source melts the material at the exact point where it is added.
The process goes by several names. Meltio calls it Wire-Laser metal deposition, or W-LMD. Research institutes such as Fraunhofer IAPT write it as DED-LB/w: directed energy deposition with a laser beam and wire. You will also see laser wire DED and Wire-Laser LMD. They all describe the same combination of laser energy and wire feedstock.
DED processes differ in two ways: the energy source (laser, electric arc or electron beam) and the feedstock (wire or powder). Wire-Laser DED sits between the arc processes, which deposit fast but with less control, and the powder processes, which give fine detail but need powder handling.
How the process works
In a Meltio deposition head, the wire is fed through the center and several lasers are arranged symmetrically around it. The lasers converge on the tip of the wire and on the surface below, creating a small melt pool.
The wire enters that melt pool coaxially, so the head deposits the same way whichever direction it moves. Meltio holds a patent on this multi-laser head with coaxial wire feed.
A typical build in five steps
Step 1: Prepare the toolpath
A slicer turns the CAD model into deposition paths: Meltio Horizon for the M600, Meltio Space for robots, or CAM software from Meltio's software partners for hybrid CNC work.
Step 2: Deposit layer by layer
The head moves along the path while the wire feeds into the melt pool. On robots and 5-axis machines it can build on curved surfaces or on existing parts.
Step 3: Shield the melt pool
Argon is delivered locally at the nozzle to prevent oxidation. The M600 goes further, with a fully inert print chamber and on the Meltio Robot Cell with Meltio inert bubble.
Step 4: Control the process
Meltio systems monitor electrical continuity between wire and part, and a load cell in the head keeps deposition within range. The Meltio M600 and the Meltio Engine Blue add a melt pool camera.
Step 5: Finish the part
The result is a near-net-shape part with a small stock allowance, machined to final tolerance and heat treated when the material requires it.
Blue and infrared lasers
The wavelength of the laser changes how much energy the metal absorbs. Meltio has built two generations of deposition head: an infrared head launched in 2019 and a blue-laser head launched in 2024, which now equips all current Meltio systems.
Blue laser head
- Generation
- Second, launched in 2024
- Lasers
- 9 direct diode lasers at 450 nm
- Total power
- 1,000 W on the M600; 1,000 or 1,400 W on the Meltio Engine Blue kits
- Main advantage
- Higher absorption: 70% more deposited volume per hour on average than the infrared head, with less laser power and a wider material range
- Materials
- Steels, nickel alloys, titanium, copper alloys and more; CuCrZr and aluminum in development
Infrared (IR) head
- Generation
- First, launched in 2019
- Lasers
- 6 fiber diode lasers at 976 nm (6 × 200 W)
- Total power
- 1,200 W rated; published print profiles run at 1,100 W
- Main advantage
- Proven for repair, good angle of attack on multi-axis systems, low-cost wear parts
- Materials
- Stainless, carbon and tool steels, nickel alloys, titanium and more
Why wavelength matters
In the near infrared, metals reflect most of the light that reaches them. A blue photon at 450 nm carries about 2.76 eV, against 1.27 eV at 976 nm, enough to trigger absorption mechanisms that infrared light cannot reach in some metals. Copper is the clearest case: its threshold sits at about 2 eV (620 nm), so it absorbs roughly 15 times more blue light than infrared.
- CopperGain: ×15
- NickelGain: ×2.1
- AluminumGain: ×2.0
- Stainless steel 304Gain: ×1.6
- TitaniumGain: ×1.3
Absorptivity of polished metals at room temperature, from NASA TN D-5353 as reproduced in Meltio's materials characterization handbook. Reading uncertainty ±2 percentage points. During printing, absorptivity is higher and depends on temperature and melt pool geometry.
More energy reaches the melt pool
For the same laser power, a metal that absorbs more turns more of that power into heat in the wire and the melt pool, so it takes less energy to deposit the same volume.
A steadier melt pool
With highly reflective metals under infrared light, melting only starts once a keyhole forms locally. The transition is abrupt, the pool is unstable, spatter increases and the process window is very narrow. At 450 nm the metal absorbs enough from the start to hold a stable conduction mode.
Copper becomes printable
For copper the question is whether it prints at all. At 5% absorption, an 1,100 W infrared head cannot form a stable, repeatable bead.
Aluminum is a different case. It already absorbs more infrared light than copper (8%), and even in blue (16%) it is the least absorbent metal in the portfolio. Absorption helps, but its low melting point and high thermal conductivity matter as much, which is why aluminum parameters are still in development.
Blue vs infrared: what Meltio's data shows
Most published research on Wire-Laser DED looks at one alloy processed with one wavelength, almost always in the near infrared. In August 2026, Meltio's Process Department compared the published material portfolio of both heads, drawing on the same laboratories and the material datasheets, and presented the results at ICAM 2026, ASTM International's additive manufacturing conference.
Twelve materials are in the portfolio and eight have a print profile on both heads. The blue profiles run at 1,000 W and the infrared profiles at 1,100 W, so the blue head works with 9% less optical power.
More deposited volume per hour on average with the blue head, from +33% to +133% across the eight materials.
Optical energy per cubic millimeter on average. The reduction ranges from 31% to 61% and appears in every material.
Minimum relative density across all nine blue-laser profiles. Two of the eight infrared profiles fall below it.
Materials with a blue-laser profile, against 9 of 12 for infrared. Only the blue head has profiles for copper and aluminum alloys.
Volume rate by material and laser head
Hover or tap a material to compare the two heads.
See the data as a table
| Material | IR 1,100 W (cm³/h) | Blue 1,000 W (cm³/h) | Blue 1,400 W (cm³/h) | Energy, IR (J/mm³) | Energy, blue 1,000 W (J/mm³) | Energy reduction |
|---|---|---|---|---|---|---|
| Ti-6Al-4V | 32.5 | 75.6 | 104.8 | 122 | 48 | −61% |
| Nickel 625 | 28.6 | 59.5 | 75.8 | 139 | 60 | −56% |
| Mild steel ER70S | 21.5 | 42.3 | 53.9 | 184 | 85 | −54% |
| Marine bronze | 24.8 | 42.5 | 110.0 | 160 | 85 | −47% |
| Tool steel H11 | 21.6 | 30.7 | 39.3 | 183 | 117 | −36% |
| Stainless 316LSi | 32.4 | 45.6 | 60.5 | 122 | 79 | −35% |
| Nickel 718 | 32.4 | 45.1 | 75.8 | 122 | 80 | −35% |
| Stainless 17-4PH | 25.3 | 33.5 | 43.9 | 157 | 107 | −31% |
| Stainless 308L | No profile | 36.7 | 60.5 | n/a | n/a | n/a |
| Invar 36 | 21.6 | No profile | No profile | n/a | n/a | n/a |
Specific energy E = 3.6 × P / Q, where P is the nominal optical power in W and Q the volume rate in cm³/h. CuCrZr (36 to 73 cm³/h) and AlSi10Mg (60 to 156 cm³/h) are blue-only profiles in development, measured mostly on thin walls, so they are not comparable with the solid profiles above.
Strength and density
Higher speed does not cost density. All nine materials with a blue-laser profile reach 99.8% relative density or higher, measured by micrograph. In the infrared, ER70S and Invar 36 stay at 99.2%.
Four materials have tensile data for both heads, all measured in the build direction (XZ), the least favorable orientation. Blue gives higher ultimate tensile strength in three of them: +75 MPa in ER70S, +71 MPa in 17-4PH and +41 MPa in Nickel 718. In 316LSi the scatter makes the difference inconclusive. Yield strength is also higher in blue in three of four, by up to +148 MPa in ER70S; Nickel 718 is the exception, 17 MPa lower. After heat treatment, Nickel 718 keeps its strength advantage in blue: 1,290 ± 26 MPa against 1,208 ± 49 MPa, with similar elongation.
The highest published tensile strength on the blue head meets or exceeds the guaranteed minimum of the feedstock wire in seven of eight materials, by 3% to 21%. The infrared head falls short of it in three of seven.
The point in favor of infraredElongation is where infrared leads. Three of the four materials tested on both heads show higher as-printed elongation in the infrared: in 316LSi, 41 ± 4% against 17.7 ± 15% in blue. Heat treatment narrows the gap to 62 ± 2% against 46 ± 14% without closing it. Nickel 718 goes the other way, with 31% in blue against 25% in the infrared. No fatigue data has been published for the blue head yet, so treat elongation as a design input when you choose a head.
What absorption does and does not explain
Absorption explains why the blue head can print reflective metals. It does not explain how much each material gains. Titanium has the smallest optical gain in the set (×1.3) and the largest energy reduction (61%). The four steels share the same optical gain and spread over 22 percentage points of reduction.
The infrared profiles run at 122 to 184 J/mm³ and the 1,000 W blue profiles at 48 to 117 J/mm³, so the two heads sit at different points of the process window. Material by material, the size of the gain depends on that window and on each alloy's thermal properties.
How to read these figures
- The study compares two generations of head, not wavelength alone: emitter count, beam shape and platform also differ.
- The test campaigns are not identical. The blue system tests 16 tensile specimens per block and the infrared system 48.
- All values are nominal figures from Meltio's own datasheets and handbook, with no statistical testing and no independent verification.
- Six of the twelve materials do not yet have full characterization on both heads.
Part quality
Wire-Laser DED builds parts that meet or exceed traditional manufacturing standards: fully dense, close to final shape and with a fine microstructure. Every Meltio Material is tested by independent laboratories with CT scans, micrography and tensile testing.
Fully dense parts
Density Verified Profiles give parts with no defects detectable by CT scanning. Utility Printing Profiles print faster for parts where minor defects have little effect.
Material efficiency
Every millimeter of wire is melted and deposited. No overspray, no powder to sieve or recycle, and standard 0.8 to 1.2 mm welding wire as feedstock.
Near-net shape
Parts are printed with minimal overbuilding, so finishing is a short machining pass. On a CNC with a Meltio Engine, printing and machining happen in the same setup.
Low heat input
The lasers concentrate the heat in a small area. That keeps the heat-affected zone small and residual stress low, which reduces warping.
Fine microstructure
Rapid solidification typically gives fine grain sizes, which add strength and toughness. Heat treatment then tailors the properties to the application, from stress relief to age hardening.
Wire-Laser DED vs other metal manufacturing processes
Wire-Laser DED is a complementary process. It sits between high-resolution powder AM and large-scale conventional manufacturing, and fits when a part is too large, too material-heavy or too time-critical for powder systems, yet needs more precision than arc deposition can give.
Where it fits
Fine detail, limited scale
Excellent for small, intricate parts, but build volume, material cost and powder handling make it inefficient for larger parts.
Fast, but coarse
Deposits large volumes quickly, but lacks the precision that complex geometries and detailed features need.
Proven, but slow and wasteful
Machining, casting and forging are reliable at volume, but long lead times, tooling and material waste weigh on low volumes and spare parts.
The bridge between them
- Wire feedstock efficiencyEvery millimeter of wire ends up in the part.
- Laser-based process controlEnergy input independent of the wire feed.
- Open material flexibilityMeltio Materials or commodity welding wire.
Process by process
| Wire-Laser DED (Meltio) | WAAM (wire arc) | EBAM (electron beam, wire) | Powder laser DED | Laser powder bed fusion | |
|---|---|---|---|---|---|
| Energy source | Several lasers around the wire | Electric arc between wire and part | Electron beam | Laser | Laser scanning a powder bed |
| Feedstock | Welding wire | Welding wire | Welding wire | Metal powder blown into the melt pool | Metal powder spread in layers |
| Material efficiency | Close to 100%: all the wire is deposited | High | High | Lower; part of the powder misses the melt pool | Unused powder must be sieved and recycled |
| Working environment | Enclosed cell or chamber with local or full inert gas | Robot cell with shielding gas | Vacuum chamber | Enclosed cell with inert gas | Sealed chamber with inert gas |
| Deposition rate | About 20 to 110 cm³/h in Meltio's published profiles | Typically 2 to 8 kg/h | Typically over 18 kg/h (40 lb/h) in titanium | Depends on system | Slower; melts powder point by point, layer by layer |
| Multimateriality | Any wire and automated dual material printing process | Any wire | Any wire | One wire | One wire |
| Resolution and control | Energy independent of wire feed; higher resolution than WAAM | Arc tied to the wire; harder to control, more spatter | Closed-loop control of beam power | Depends on system | Finest detail of the five |
| Heat input | Small heat-affected zone, about one previous layer | Higher; more warpage and residual stress | High power, typically 5 to 20 kW | Depends on system | Depends on material and scan strategy |
| Typical part size | About 50 mm to over 1 m | Large, up to several meters | Large, up to about 5.8 m (19 ft) | Depends on system | Mostly small to medium; large-format machines exist |
| Repair and feature addition | Yes, on existing parts and in hybrid CNC | Yes | Yes | Yes | No |
| Operator exposure to powder | None | None | None | Yes, powder handling required | Yes, powder handling required |
Sources: Meltio technology, materials and FAQ pages; Meltio Process Department wavelength study (ICAM 2026); MX3D, WAAM3D and Sciaky public figures; Fraunhofer IAPT on WAAM. Competitor figures are those companies' own published claims and are given in kg/h, while Meltio's are volume rates.
Powder bed fusion
PBF excels at small, detailed parts with fine resolution, and stays a strong option for compact parts where its cost and powder handling are justified. It meets limits when parts grow:
- Machine envelope caps part size
- High material cost of fine powder
- Operational complexity: powder recycling and safety
- Long qualification cycles
Wire-Laser DED
Preferred for larger components and industrial integration:
- Beyond PBF size limits, from about 50 mm to over 1 m
- Near-net shape cuts machining time
- Wire feedstock: lower waste, no powder logistics
- Suited to repair and hybrid manufacturing
Powder-based DED
Offers large build volumes, but keeps the drawbacks of powder:
- Lower material utilization and overspray
- Contamination risk and oxidation sensitivity
- Complex powder handling requirements
- Powder flow variations that affect melt pool stability
Wire-Laser DED
Wire feedstock removes the powder limitations:
- Close to 100% material efficiency
- No overspray and no powder waste
- Stable, predictable material input
- Simpler material qualification
WAAM
Wire arc AM deposits faster and its equipment usually costs less, which makes it valuable for very large, simple structures. Its limits show on detailed parts:
- Higher heat input: more distortion, warpage and residual stress
- Large melt pools make dimensional control harder
- Lower resolution and rougher surfaces
- Heavier reliance on machining
Wire-Laser DED
The laser gives a balance between WAAM and powder processes:
- Localized energy and precise control of heat input
- Higher resolution: finer features and better surface quality
- Wire efficiency that keeps the process industrially scalable
- Consistent mechanical properties in detailed parts
EBAM
Electron beam AM also uses wire and reaches very high deposition rates, especially in titanium. But:
- It needs a vacuum chamber
- Part size is limited to the chamber
- The process is tied to a fixed installation
Wire-Laser DED
Works with local shielding gas or an inert chamber, so it installs where the work is:
- On an industrial robot
- Inside a CNC machining center
- In a deployable container or on a ship
Traditional manufacturing
Machining, casting and forging remain the reference for series production. For low volumes, spares and repairs they bring:
- Lead times of many months
- Material waste and costly tooling
- Limited design flexibility and slow iteration
Wire-Laser DED
Competes directly in specific, high-value cases:
- Lead times from months to weeks or days
- Near-net shape reduces material waste
- Feature addition and life-extending repairs on existing parts
Example · Parts with a high buy-to-fly ratio
For low to medium volume casting replacement in Stainless Steel 316L, a hybrid process prints the part close to shape and machines only the functional surfaces. Internal curved features that are impossible or expensive to machine are left as printed.
The right tool, not a universal replacementWire-Laser DED is the right approach when flexibility, speed and material efficiency give a clear advantage: when WAAM is too coarse and powder systems are inefficient for the part.
Materials
Wire-Laser DED prints a wide range of alloys available as welding wire, from 0.8 to 1.2 mm in diameter on Meltio systems. Each Meltio Material has its own datasheet and tested print profiles.
Stainless steels
- Stainless Steel 316L
- Stainless Steel 308L
- Stainless Steel 17-4PH
Carbon and tool steels
- Mild Steel ER70S
- Tool Steel H11
Nickel and iron-nickel alloys
- Nickel 718
- Nickel 625
- Invar
Titanium, copper and aluminum
- Titanium 64 (Ti-6Al-4V)
- Marine Bronze ERCuNiAl
- CuCrZr (in development)
- Aluminum 4046 (in development)
Systems with dual or quad wire switch between up to four materials in the same part, for example a tough core with a wear-resistant surface. The copper and aluminum alloys need the blue-laser head.
Beyond the Meltio Materials portfolio
Meltio runs an open material platform: you can print Meltio-validated wire or certified third-party commodity wire, with no paid unlocking or licence fees. Alongside Meltio Materials, these alloys have been printed successfully with infrared and blue laser systems. They are not part of the pre-parameterized portfolio, so each one is developed for the application.
| Family | Alloys | Typical applications |
|---|---|---|
| Stainless steels and duplex | Martensitic 410, 420 · Austenitic 307, 309 · Nitronic 50 · Super Duplex 2507 | Valves and marine components (Super Duplex); oil and gas, defense and food industry (307, 309) |
| Tool and low-alloy steels | Tool steel H12, H13, P20 · AISI 4130, AISI 8260 | Hot work tooling, die casting and molding |
| Titanium and cobalt alloys | Ti Gr. 5553, Ti Gr. 23 · Haynes 25, Stellite 6, MP35N | Motorsports and defense (Ti 5553); wear-resistant valves, pump components and gas turbines (Stellite 6, Haynes 25) |
| Nickel alloys and specialty | Hastelloy X, Monel K500 · Nitinol · Tungsten carbide (NiCarbW) | Aerospace, petrochemical and energy (Hastelloy X); marine and propeller shafts (Monel K500); shape-memory parts for medical and aerospace (Nitinol); wear-resistant coatings for mining and construction (tungsten carbide) |
| Bronze alloys and noble metals | Silicon bronze (ERCuSi-A) · Bearing bronze · Pure, white and red gold | Electrical and marine components (silicon bronze); electronics and jewelry (gold) |
| White metal, refractory metals and aluminum | Babbitt NB90 · Niobium · AL-6063, AL-5158, Scalmalloy | Bearing linings (Babbitt) |
What Wire-Laser DED is used for

New near-net-shape parts
Parts that would be cast, forged or machined from billet, printed close to final shape and then finished. ASRI and AMT3D printed two 500 mm Ti-6Al-4V rings for a launch vehicle using segmented M600 builds. Mol-Matric, within the SAFE-AIR project, turned three aluminum parts into a single titanium part on the M600.
Read the titanium rings use case
Repair and cladding
Rebuilding worn areas and applying wear-resistant layers instead of replacing the part. An industrial pump repair saved 70% of the cost and cut lead time from two months to one week, and trencher blades were hardfaced with dilution below 10%.
Read the hardfacing use case
Hybrid manufacturing
Printing and machining in the same CNC setup, adding material only where it is needed. Meltio's partner Phillips Corporation integrates the Meltio Engine into Haas machining centers.
See the Meltio Engine for CNC
Spare parts at the point of need
Producing parts close to where they are used, including on ships and in deployable containers. The British Army and Plastometrex reprinted and tested a vehicle brake pedal in the field.
Read the brake pedal use case
Use case · Oil and gas
ExxonMobil moved titanium components to Wire-Laser DED at its Baton Rouge refinery.
Read the ExxonMobil use caseIs your part a good fit?
- Medium to large size, roughly from 50 mm to over 1 m, where powder bed fusion becomes too slow or expensive.
- It needs material added to an existing part: flanges, features on shafts or repairs.
- It is made from an expensive or hard-to-machine metal such as titanium, Inconel or tool steel, where machining from billet wastes most of the material.
- Moderate complexity, typical of cast or forged parts, with walls thicker than 2.0 mm.
If a part is too large for powder bed fusion, too precise for WAAM and too wasteful or slow to machine, Wire-Laser DED is likely the right process.
Ask for an application assessmentHow to adopt Wire-Laser DED
Use the process as a standalone machine, add it to equipment you already own or work through a partner. All current Meltio systems use the blue-laser head.

Meltio M600
Standalone industrial printer with a 300 × 400 × 600 mm inert build chamber and a 1,000 W blue-laser head, designed to run unattended in production.
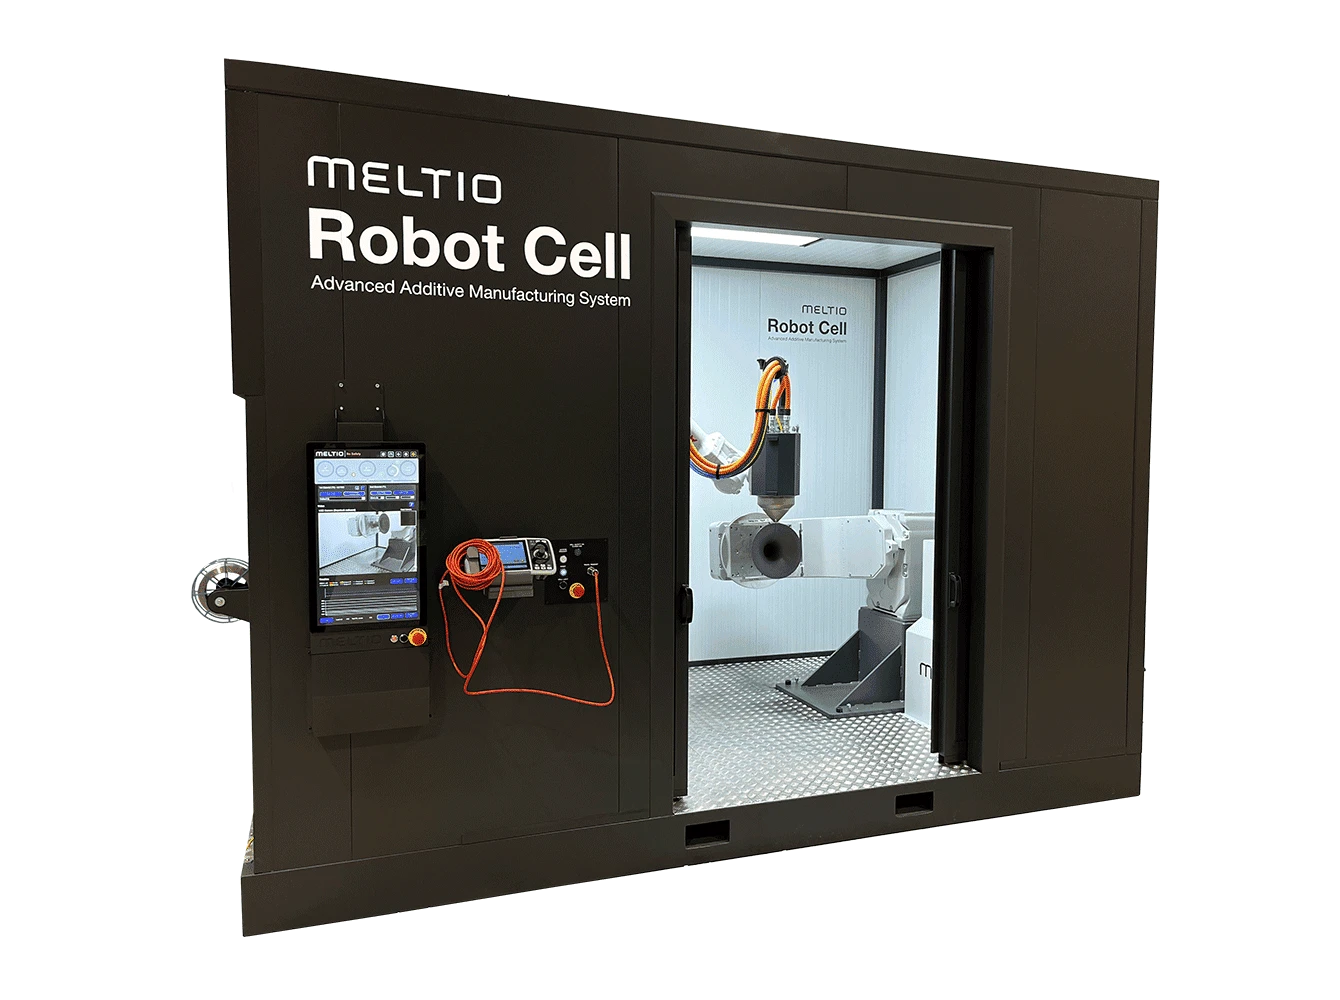
Meltio Robot Cell
Turnkey 8-axis robotic cell with the Meltio Engine Blue head for large parts and repair, delivered integrated and tested.
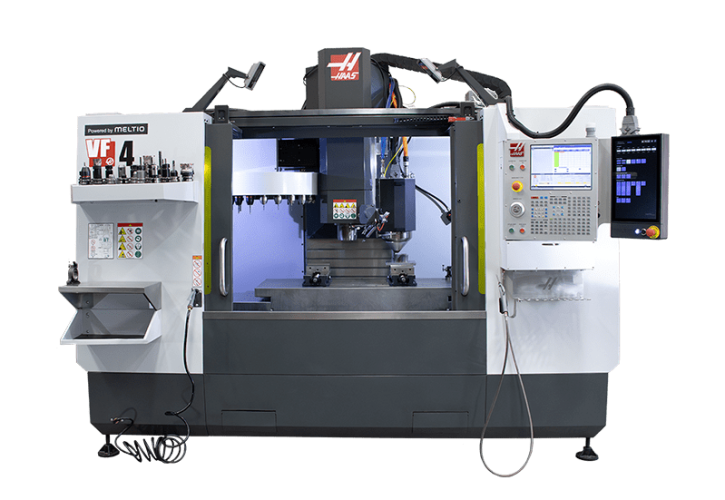
Meltio Engine for CNC
Kit with a 1.0 or 1.4 kW blue-laser head that adds Wire-Laser deposition to a machining center for hybrid manufacturing.

Meltio Engine for industrial robots
Kit with a 1.0 or 1.4 kW blue-laser head to turn an existing robot arm into a metal printing system, with a build volume limited only by the robot's reach.

Powered by Meltio
Complete solutions built and validated by Meltio's certified integration partners: robot cells, hybrid CNC machines and containerized systems.
Frequently asked questions
Is Wire-Laser DED the same as laser metal deposition (LMD)?
Wire-Laser DED is laser metal deposition that uses wire as feedstock. LMD is the broader term and also covers processes that blow metal powder into the laser. Meltio's process is sometimes written as W-LMD or wire-LMD to make the difference clear.
Is Wire-Laser DED faster than WAAM?
No. WAAM deposits material faster. Wire-Laser DED gives more precise process control, a smaller heat-affected zone and higher resolution, so it suits parts that need more accuracy than WAAM can deliver.
What deposition rate does Wire-Laser DED reach?
In Meltio's published print profiles, volume rates range from about 21 cm³/h on the infrared head to 110 cm³/h on the 1,400 W blue head, depending on the material. On the 1,000 W blue head of the Meltio M600 they range from 30.7 cm³/h in H11 tool steel to 75.6 cm³/h in Ti-6Al-4V.
Can Wire-Laser DED produce fully dense parts?
Yes. With Meltio's Density Verified Profiles, printed parts show no defects detectable by CT scanning. On the blue-laser head, all nine materials with a published profile reach a relative density of 99.8% or higher.
Do Wire-Laser DED parts need machining?
Usually yes, on functional surfaces. The process builds near-net-shape parts with a small stock allowance, which is then machined to final tolerance. On a CNC machine fitted with a Meltio Engine, printing and machining happen in the same setup.
Which metals can be printed with Wire-Laser DED?
A wide range of alloys available as welding wire. Meltio's portfolio includes stainless steels, mild steel, tool steel H11, nickel alloys 718 and 625, Titanium 64, Invar, marine bronze, and CuCrZr and an aluminum alloy, both in development on the blue-laser head.
Is a blue laser better than an infrared laser for Wire-Laser DED?
On most measures in Meltio's published data, yes. Across the eight materials profiled on both heads, the 1,000 W blue profiles deposit 70% more volume per hour on average than the 1,100 W infrared profiles and need 44% less optical energy per cubic millimeter, with no loss of density. Infrared keeps one advantage: higher as-printed elongation in three of the four materials tested on both heads.
Can Wire-Laser DED print copper?
Pure copper and high-copper alloys need a blue laser. Polished copper at room temperature absorbs about 5% of infrared light at 976 nm and about 75% of blue light at 450 nm. At 5%, an 1,100 W infrared head cannot form a stable, repeatable bead. Meltio's CuCrZr profile for the blue head is in development; marine bronze, a copper-nickel-aluminum alloy, already prints on both heads.
Is Wire-Laser DED safe to use in a normal workshop?
Meltio systems are Class 1 laser products that run enclosed, and wire removes the risks of handling fine metal powder. Installation still needs the right electrical supply, inert gas and, for robot integrations, a laser-safe cell.
Go deeper
- What is laser metal depositionLMD with wire and powder, and how it compares with WAAM and SLM
- Wire arc additive manufacturingHow WAAM works, its limits and where it fits
- Powder DED technologiesBlown-powder deposition and how it differs from wire
- The benefits of a wire-based processWhy wire is the feedstock for Meltio systems
- Hybrid manufacturingCombining deposition and machining in one setup
- Repair strategies with wire-LMDPlanning repairs and cladding on worn parts
- Near-net shape and over-thicknessHow much stock to leave for machining
- Wire-Laser materials guideProperties and uses of each alloy
- Dual wire printingTwo materials in the same part
See if Wire-Laser DED fits your parts
Send us a drawing or describe your part, material and volumes. An application engineer or your local partner will tell you whether it is a good candidate and which system fits.