
TNB Remaco Prints an Open Impeller for Power Generation and Oil & Gas

TNB Remaco supports critical assets across power generation and Oil & Gas, industries where a stalled pump or compressor is not a minor inconvenience. It is lost output. When an impeller fails, the conventional route can involve sourcing a replacement from the OEM or commissioning a new part through casting and CNC machining, with lead time depending on material availability, supplier capacity and machining requirements.
TNB Remaco wanted to explore whether metal additive manufacturing could provide an additional route for low-volume, high-value or time-critical spare parts, while maintaining the reliability and engineering discipline required for industrial applications.
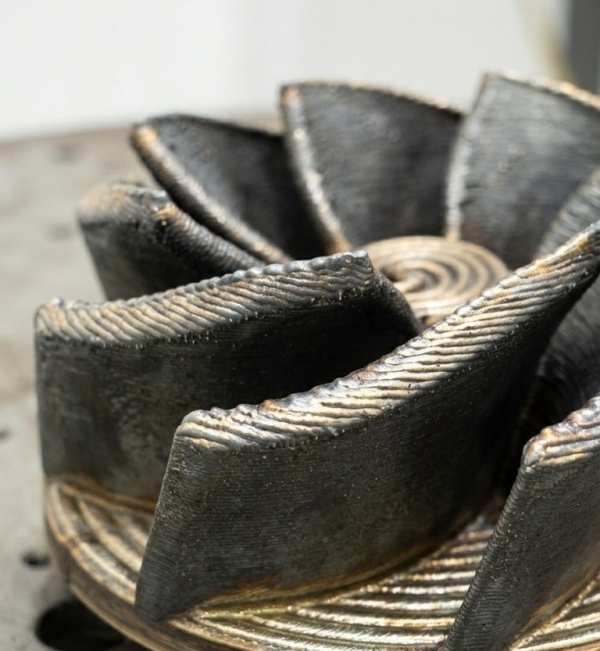
The team reverse-engineered an open impeller, produced it in stainless steel 316L using Meltio’s wire-laser metal deposition process, and then applied CNC machining to achieve the required final geometry. The project became an important proof point for a broader manufacturing capability that TNB Remaco is now building in-house.
What the team wanted was simple: low-volume, high-value or time-critical spare parts, while maintaining the reliability and engineering discipline required for industrial applications.
1. The part that can’t sit on a shelf
An open impeller transfers energy into the working fluid inside pumps and compressors, and TNB Remaco supports plants where reliable operation of this equipment is critical. When a component degrades or fails, the equipment may remain unavailable until a suitable replacement is manufactured and delivered.
For this project, the conventional manufacturing route involved sourcing material followed by machining. TNB Remaco experienced approximately one month for material sourcing and another month for machining, creating a lead time of around two months before the part was ready for the next stage.
For critical or obsolete components, particularly where original drawings may no longer be available, the ability to reverse-engineer the part and establish an alternative manufacturing route can be valuable.
TNB Remaco has been developing spare parts through reverse engineering for many years, using conventional processes such as casting, machining, welding, surface treatment and heat treatment. The objective is not to replace these technologies, but to add another option where it provides a technical or lead-time advantage.
The strategy is simple: manufacture when a part is unavailable, and repair when a part can be economically restored. This impeller sits on the manufacturing side of that strategy.
2. A hybrid build: print near-net-shape, finish on CNC
TNB Remaco’s position is that every manufacturing technology has its place. Casting remains an effective solution for suitable applications, particularly where production volume justifies tooling and process preparation. CNC machining provides the dimensional accuracy and surface finish required for precision components. For selected low-volume or complex parts, wire-laser metal deposition such as Meltio offers another route to produce material close to the required final geometry before machining.
For this impeller, TNB Remaco reverse-engineered the geometry and produced a near-net-shape component in SS316L using Meltio’s wire-laser deposition process. The deposited component was then finish-machined using CNC equipment to achieve the required dimensional tolerances and surface finish.
This additive-plus-subtractive sequence is central to TNB Remaco’s approach: additive manufacturing does not replace machining; it works together with machining to provide a practical manufacturing route.
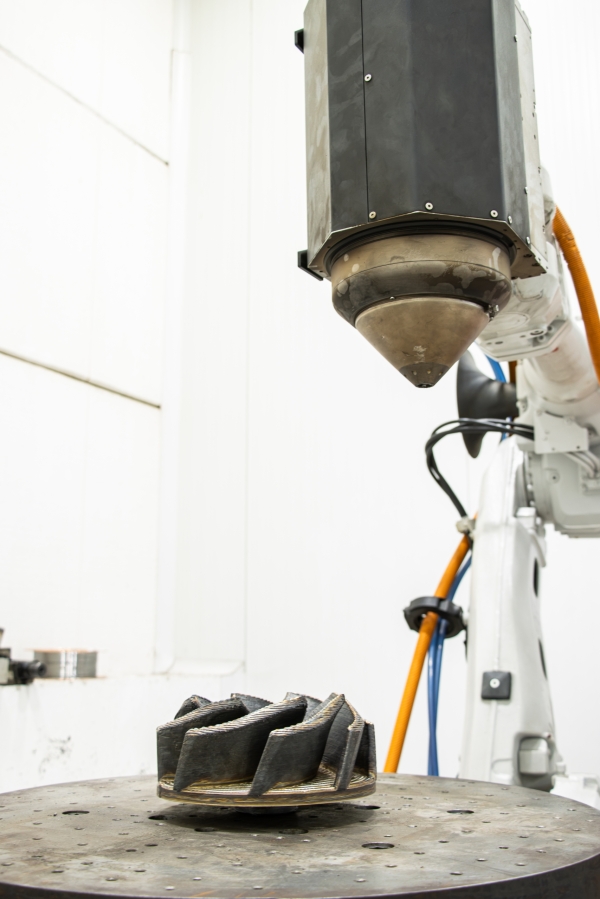
TNB Remaco is implementing a Meltio Robot Cell for this capability. The robotic configuration provides the flexibility to plan deposition strategies around different component geometries and also supports future applications such as repair and cladding. The process uses welding wire rather than metal powder. This fits naturally with TNB Remaco’s existing welding and fabrication environment, while providing access to commonly available industrial wire materials.

3. What the impeller proves, and what’s still being checked
The finished impeller weighs approximately 11 kilograms.
More importantly, the project demonstrated a complete manufacturing workflow from reverse-engineered geometry through metal additive manufacturing and CNC finishing. The impeller is being treated as a demonstration and validation component, rather than being assumed ready for service simply because it has been successfully printed.
Further inspection and testing are part of the qualification process. Penetrant inspection is planned after machining to check for surface-breaking defects, while mechanical property testing is scheduled to establish the material performance before the component is considered for full service.
For TNB Remaco, this qualification approach is essential. Additive manufacturing must meet the same engineering expectations as any other manufacturing route for components intended for industrial equipment.
Wire-laser metal deposition fits this job well: the project demonstrated a complete manufacturing workflow from reverse-engineered geometry through metal additive manufacturing and CNC finishing.
4. The start of a bigger capability
For TNB Remaco, this impeller is not a one-off exercise. It is an early demonstration of a broader manufacturing capability that brings together reverse engineering, 3D scanning, additive manufacturing, CNC machining, metallurgy and inspection as one connected process. The objective is to develop the capability to select the most appropriate manufacturing route for each spare part — whether that means casting, machining, welding, additive manufacturing, repair, or a combination of processes.
The initial focus is power generation, with potential application across the Oil & Gas, petrochemical, marine and heavy engineering sectors supported by TNB Remaco.
As industrial assets continue to age and some components become obsolete or difficult to source, operators increasingly need alternatives to simply maintaining large inventories of critical spares. For TNB Remaco, the longer-term opportunity is to combine reverse engineering and digital part information with flexible manufacturing technologies to support just-in-time manufacturing and faster response for critical spare parts.
The goal is not simply to print parts. It is to build the engineering capability to understand the material, understand the geometry, select the right manufacturing process, and validate the finished component.
That is the foundation for TNB Remaco’s next generation of spare-part manufacturing.
FAQs
An open impeller is a rotating component used inside pumps and compressors to transfer energy to a fluid. TNB Remaco reverse-engineered and produced an open impeller in SS316L using metal additive manufacturing to explore an alternative manufacturing route for low-volume and potentially time-critical industrial spare parts.
The project is also a proof point for TNB Remaco's broader capability combining reverse engineering, additive manufacturing, CNC machining, metallurgy and inspection.
TNB Remaco sees additive manufacturing as an additional manufacturing route rather than a replacement for casting or CNC machining. For selected low-volume, complex or time-critical parts, wire-laser deposition can produce a near-net-shape component without requiring the same manufacturing route as a conventional cast component.
CNC machining is then used to achieve the required dimensional tolerances and surface finish.
The impeller was produced in SS316L stainless steel for this demonstration. Material selection for future components will depend on the specific application and requirements, including operating temperature, corrosion resistance, wear resistance, mechanical properties and the specification of the original component.
For this project, the conventional route involved approximately one month for material sourcing followed by another month for machining. The additive manufacturing route provided an alternative approach by producing the component directly from wire through deposition, followed by CNC finishing.
The exact production lead time for the complete additive route will depend on the component geometry, deposition strategy, material, machining requirements and inspection/qualification requirements.
TNB Remaco is implementing a Meltio Robot Cell based on a robotic wire-laser metal deposition process. The robotic configuration provides flexibility for different component geometries and future applications including manufacturing, repair and cladding. Furthermore, the size of printing envelop of Diameter 1.4m x height 1m fits very well with most of the Power Generation parts sizes.
The system uses welding wire rather than metal powder, which fits well with TNB Remaco's existing welding and fabrication capabilities.
TNB Remaco sees this impeller as an early proof point for a broader manufacturing capability. The plan is to integrate reverse engineering, 3D scanning, additive manufacturing, CNC machining, metallurgy and inspection into a connected workflow.
The capability will initially support power generation applications, with potential expansion into Oil & Gas, petrochemical, marine and heavy engineering applications.
The longer-term objective is to support just-in-time manufacturing and faster response for selected critical, obsolete, low-volume or time-sensitive spare parts.